
Call us now :08045814454
 Send Inquiry


 Send Inquiry
Stainless Steel Chemical Reactors
Price 450000 INR/ Unit
MOQ : 1 Unit
Stainless Steel Chemical Reactors Specification
- General Use
- Industrial
- Material
- Stainless Steel
- Capacity
- 5 Kiloliter/day
- Automatic
- Yes
- Drive Type
- Electric
- Voltage
- 220-440 Volt (v)
Stainless Steel Chemical Reactors Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 10 Units Per Month
- Delivery Time
- 2-10 Days
- Main Domestic Market
- All India
About Stainless Steel Chemical Reactors
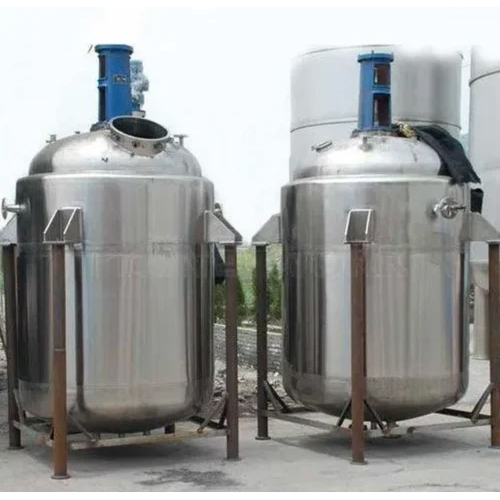
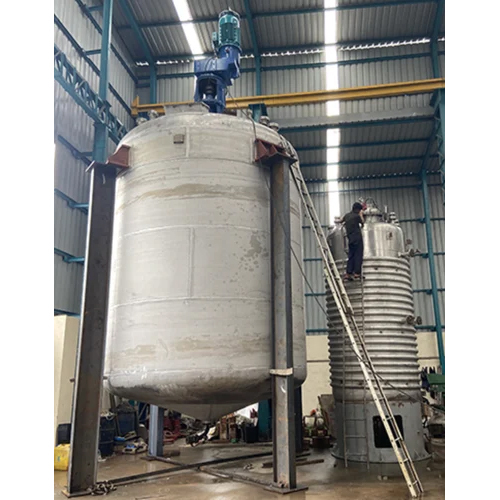
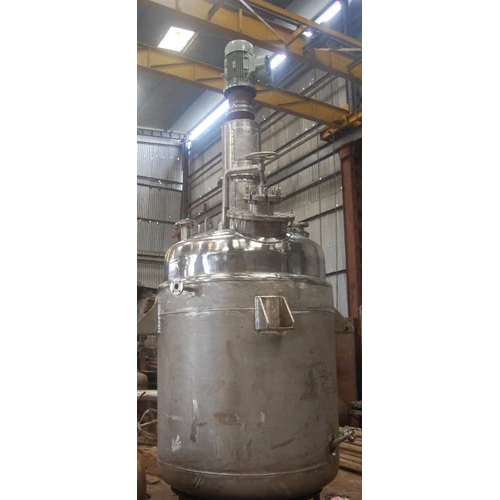
Find the preeminent solution for your industrial processing needs with our Stainless Steel Chemical Reactors. Must-have for manufacturers seeking impeccable performance, these reactors are renowned for their eminent quality and durability. Featuring a large 5 kiloliter per day capacity and electric-powered automatic operation, they cater to diverse industrial applications. Made from premium stainless steel and operating at 220-440 Volt, these reactors are trusted by industries across India for their reliable and efficient processing. Buy from the leading manufacturer and supplier to experience unmatched safety and market value.
Versatile Industrial Application and Usage
Stainless Steel Chemical Reactors are widely used by eminent manufacturers and processing plants for diverse chemical reactions and synthesis. Their robust design and impeccable durability make them ideal for petrochemical, pharmaceutical, and specialty chemical industries. These reactors are tailored for continuous and batch processes, ensuring uniform mixing and optimal reaction efficiency. Their application includes blending, distillation, and formulation, supporting superior product quality and reliable plant operation across India.
Export Ready: Stock, Certification, and Supply
Our Stainless Steel Chemical Reactors are market-ready and available with stock ready for prompt dispatch. Handed over at major Indian FOB ports, we ensure swift shipping and delivery to your plant or project site. Certified by reputed industry bodies for safety and quality, our reactors meet eminent global standards. With a substantial supply ability, we guarantee to fulfil bulk orders efficiently, enhancing market value and reliability for your industrial expansion.
Versatile Industrial Application and Usage
Stainless Steel Chemical Reactors are widely used by eminent manufacturers and processing plants for diverse chemical reactions and synthesis. Their robust design and impeccable durability make them ideal for petrochemical, pharmaceutical, and specialty chemical industries. These reactors are tailored for continuous and batch processes, ensuring uniform mixing and optimal reaction efficiency. Their application includes blending, distillation, and formulation, supporting superior product quality and reliable plant operation across India.
Export Ready: Stock, Certification, and Supply
Our Stainless Steel Chemical Reactors are market-ready and available with stock ready for prompt dispatch. Handed over at major Indian FOB ports, we ensure swift shipping and delivery to your plant or project site. Certified by reputed industry bodies for safety and quality, our reactors meet eminent global standards. With a substantial supply ability, we guarantee to fulfil bulk orders efficiently, enhancing market value and reliability for your industrial expansion.
| Capacity | 500 L |
| Storage Capacity | 10 KL |
| Material | Stainless Steel |
| Usage/Application | Industrial |
| Max Design Pressure | 15 bar |
| Automation Grade | Automatic |
FAQs of Stainless Steel Chemical Reactors:
Q: How are Stainless Steel Chemical Reactors used in industrial plants?
A: Stainless Steel Chemical Reactors are involved in a range of industrial processes, including mixing, distillation, synthesis, and formulation. Their automatic controls and robust design make them suitable for continuous as well as batch production environments.Q: What are the main benefits of using stainless steel in chemical reactors?
A: Stainless steel offers impeccable corrosion resistance, strength, and durability, which ensures a longer equipment lifespan, reduced maintenance needs, and consistent product quality even under challenging industrial conditions.Q: Where can I install these reactors within my facility?
A: These reactors are flexible for installation in various sections of a chemical plant, including synthesis, blending, and formulation units, providing efficient processing wherever placed.Q: When can the reactors be delivered after ordering?
A: With stock ready and streamlined logistics, reactors can be dispatched promptly from major FOB ports in India, ensuring timely delivery to your site upon completion of standard procedures.Q: What certifications back the quality of these reactors?
A: Our Stainless Steel Chemical Reactors come with reputable safety and quality certifications, confirming compliance with national and international industry standards for reliable performance.Technical Details 

Tell us about your requirement

Price:
Quantity
Select Unit
- 50
- 100
- 200
- 250
- 500
- 1000+
Additional detail
Mobile number
Email

More Products in Chemical Reactor Category

Chemical Industry Reactor
Price 250000 INR / Piece
Minimum Order Quantity : 1 Piece
Voltage : 220 Volt (v)
General Use : Chemical Industry
Automatic : Yes
Material : Stainless Steel

Industrial Chemical Reactor
Price 350000 INR / Piece
Minimum Order Quantity : 1 Unit
Voltage : 220 Volt (v)
General Use : Industrial
Automatic : Yes
Material : Stainless Steel

Industrial Ss Chemical Reactor
Price 400000 INR / Piece
Minimum Order Quantity : 1 Unit
Voltage : 220 Volt (v)
General Use : Chemical Industry
Automatic : Yes
Material : Stainless Steel

Stainless Steel Jacketed Reactor
Price 450000 INR / Unit
Minimum Order Quantity : 1 Unit
Voltage : 220440 Volt (v)
General Use : Industrial
Automatic : Yes
Material : Stainless Steel

 Send Inquiry
Our Products
- Stainless Steel Agitator
- Vacuum Dryer
- Nutsche Filter
- Chemical Reactor
- Vacuum Tray Dryer
- Basket Centrifuge
- Herbal Extraction and Distillation
- Fluid Bed Dryer
- U-Tube Heat Exchanger Bundle
- Mixing Impeller
- Pressure Filter
- Ribbon Blender
- Horizontal Rotary Extractor
- Stainless Steel Tank
- Storage Vessel
- Centrifuge Machine
- Mixing Vessel
- Shell and Tube Heat Exchanger
- Paddle Mixer Machine
- Steam Distillation Unit
- Falling Film Evaporator
- Multiple Effect Evaporator
- Film Evaporator
- Double Cone Blender
- Octagonal Blender
- Fluid bed dryer
- Extracting Machinery
- Blender Machine
- Plate Heat Exchanger
- Horizontal Autoclave


Plot No. A/2, Sector-A, Industrial Area, Sanwer Road,Indore - 452015, Madhya Pradesh, India

Ms. Shraya
(Chief Executive)
Mobile :08045814454
 Send Inquiry
 Call Me Free

Developed and Managed by Infocom Network Private Limited.
 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
